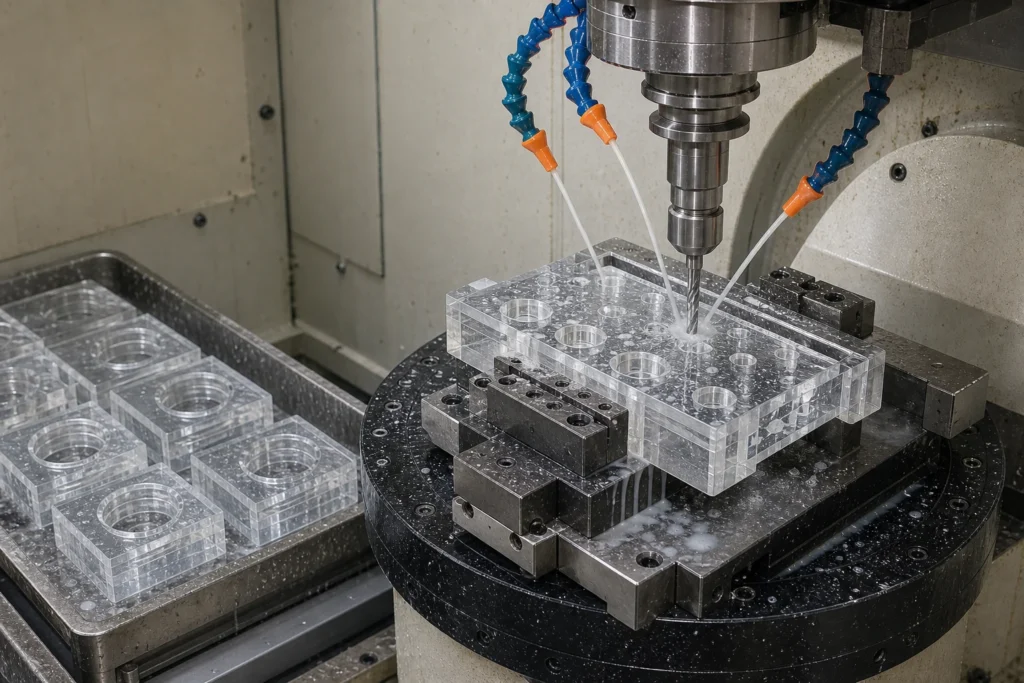
Quick answer: Drilling Fused Silica covers Fused Silica (CTE 0.55 x 10^-6 /K, 185 nm – 2.5 um); Drilling to +/-0.02 mm hole position. Prototypes ship in 5-10 working days.
We drill Fused Silica daily, in thicknesses from 0.1 – 30 mm. The controlling numbers: +/-0.02 mm hole position working tolerance, 0.15 mm laser / 0.5 mm mechanical minimum features, and exit-chip controlled below 0.1 mm off the machine. Where the drawing asks for more, downstream lapping and polishing take over.
Specifications at a glance
| Material | Fused Silica (JGS1 (UV), JGS2 (standard), JGS3 (IR)) |
|---|---|
| Thermal expansion (CTE) | 0.55 x 10^-6 /K |
| Service temperature | 1,100 C continuous |
| Transmission range | 185 nm – 2.5 um |
| Density | 2.20 g/cm3 |
| Knoop hardness | 500 kg/mm2 |
| Refractive index | 1.458 @ 587 nm |
| Stock thickness | 0.10 – 50 mm |
| Maximum blank size | 450 x 450 mm |
| Process | Drilling |
| Working tolerance | +/-0.02 mm hole position |
| Minimum feature | 0.15 mm laser / 0.5 mm mechanical |
| Surface finish | exit-chip controlled below 0.1 mm |
| Thickness window | 0.1 – 30 mm |
| Edge condition | optional chamfered hole entry |
| RFQ inputs | PDF/DXF/STEP drawing, quantity brackets, surface and edge spec |
Capabilities and limits
The core strength of Drilling is through-holes, blind holes and countersinks at densities beyond 1,000 holes per part. The honest limit: hole-to-edge distance should stay above 1.5x thickness to protect strength. Both belong on the drawing before quoting, not after.
One material, many routes: on Fused Silica we also quote sandblasting, edge grinding, ultrasonic machining, coring, and multi-step drawings are the norm rather than the exception.
Getting the drawing right
Three items decide most of the cost and lead time on this work:
- Material note: its hardness and brittleness demand diamond tooling and controlled feeds.
- Process boundary: hole-to-edge distance should stay above 1.5x thickness to protect strength.
- Over-specification is the quiet budget killer: a 20/10 scratch-dig face costs roughly three times an 80/50 face, so grade each surface individually.
For the complete framework, see the tolerance design guide and the holes and edges design guide.
Where these parts end up
drilling fused silica shows up across scientific instruments (reference flats, cells, prism mounts, stage inserts); microfluidic devices (chips, manifolds, via plates, bonded stacks); laboratory instruments (cuvettes, sight glasses, stir-cell windows). Background reading on the underlying material science: RP Photonics: fused silica.
Dimensions still moving? Configure this part live in the 3D + 2D builder below, or open the full custom glass machining 3D + 2D builder to start from a blank canvas.
Useful companion pages: CNC machining capability, material selection guide, Borofloat 33 selection guide.
Buyer questions, answered
What equipment runs the drilling work?
Diamond core drills, ultrasonic assist and laser percussion heads.
Is there a minimum order for drilling fused silica?
No. Single prototypes are accepted, and pricing steps down at 10, 100 and 1,000 pieces.
How fast can prototypes ship?
Machined prototypes ship in 5 – 10 working days. Coated or bonded parts add 1 – 2 weeks depending on queue slots.
What files do you need for a quote?
A dimensioned PDF plus DXF or STEP geometry. If only a sketch exists, our drawing review service formalizes it before quoting.
Specifications on this page were last reviewed by our engineering team in September 2026.